How to choose a cutting machine for stone based on slab thickness
Author
Date Published
Reading Time
Match the cutting machine to the finished thickness, maximum incoming thickness, and required edge quality, rather than choosing from blade diameter or motor power alone. A machine that handles thin porcelain-like stone tiles efficiently can be unsuitable for a thick granite tread, even when both pieces fit beneath the cutting head. The thicker section changes the blade engagement, feed load, clamping requirement, cooling demand, and likelihood of edge breakout.
Start by separating three dimensions that are often treated as one: the nominal slab thickness on the drawing, the actual thickness of received material, and the depth that must be cut. Calibration variation, surface texture, protective film, and warpage can make the incoming piece thicker than its stated size. A full-depth crosscut also places a different load on the machine than a shallow trimming pass on the same slab.
Use thickness bands to narrow the machine type
Thin stone tiles and panels, commonly used for wall cladding, flooring inserts, or lightweight architectural elements, need controlled support more than extreme cutting depth. A bridge saw or tile saw with a rigid, flat table and a fine continuous-rim diamond blade is often appropriate when the material is supported across the cut. Thin work can vibrate if it bridges a gap in the table, producing chips that look like a blade problem but are actually caused by poor backing support.
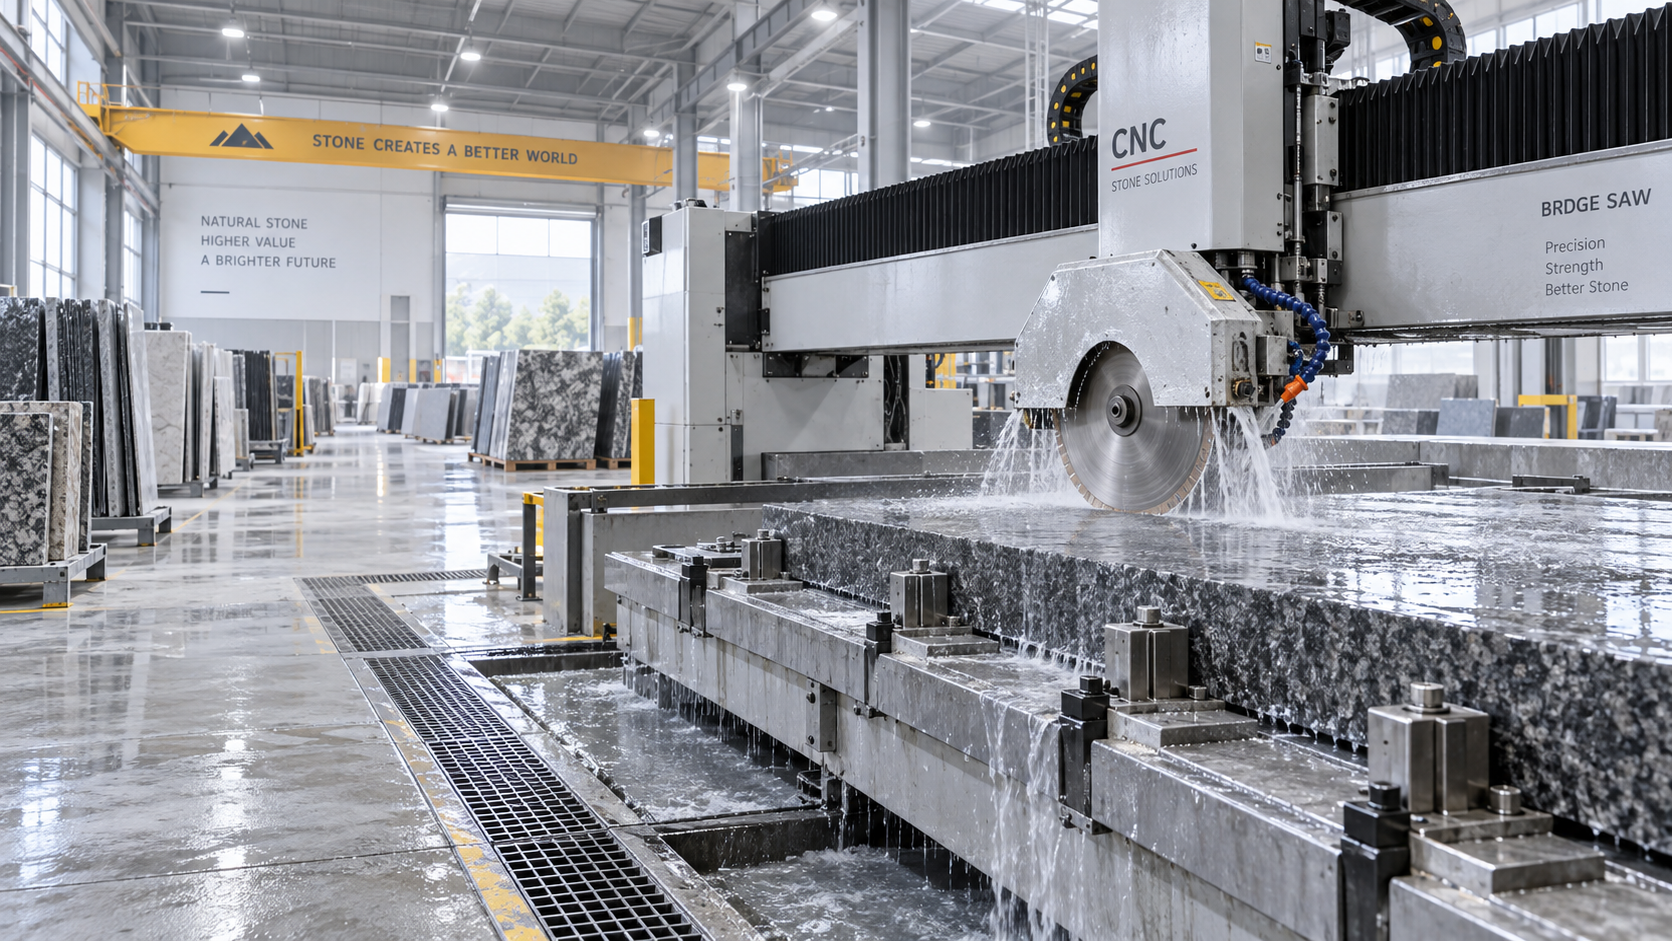
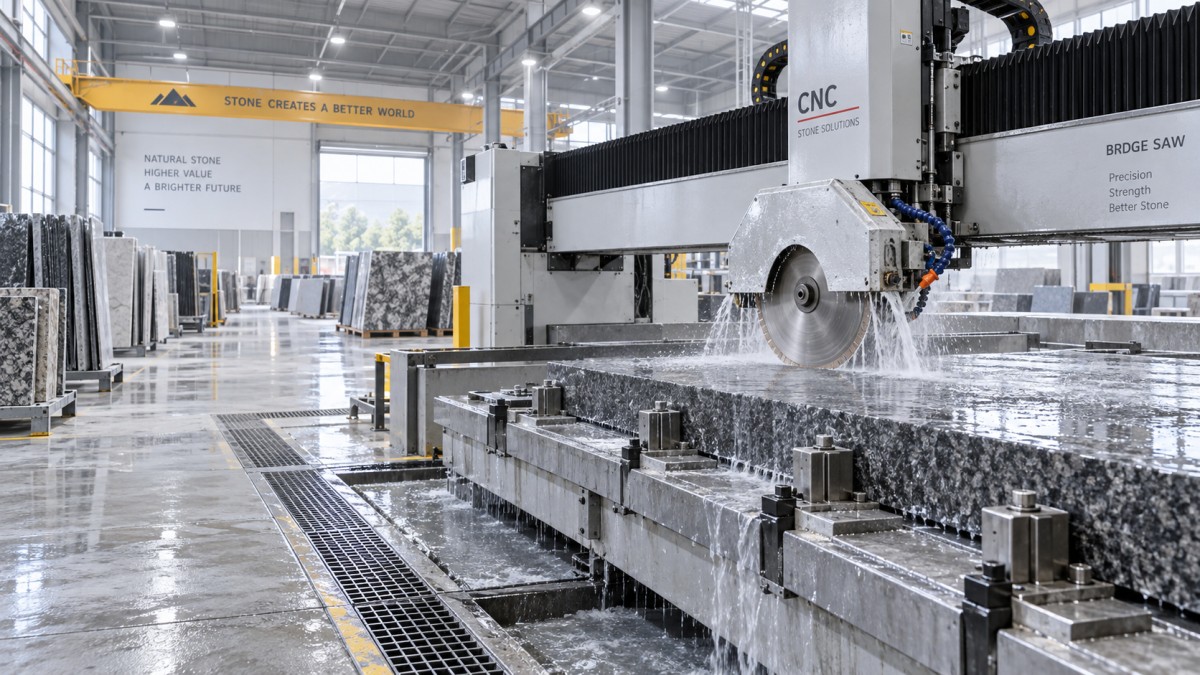
For standard slabs used in countertops, vanity tops, window sills, and similar fabricated pieces, a bridge saw remains the usual reference point. Its advantage is not simply reach. The bridge, spindle carriage, rails, and table create a stable geometry for straight cutting on wide, heavy material. This format is especially useful where cut squareness must remain consistent across long lengths or where repeated cuts need to align with downstream edge profiling and installation joints.
Heavy stone sections demand more than a larger blade. Thick granite blocks, landscaping pieces, stair treads, curbs, and engineered-stone sections require sufficient throat clearance, structural rigidity, secure positioning, and a drive system that maintains blade speed under load. A deep-cut bridge saw, block saw, or dedicated masonry saw may be appropriate according to the piece size and handling method. For irregular or very large pieces, the way the material is loaded and restrained can become the limiting factor before the rated cutting depth is reached.
Rated depth is a starting point, not the usable depth
A published maximum depth usually assumes a specified blade diameter and a favorable machine position. It does not automatically represent the depth available for a real workpiece. Blade flanges, the arbor assembly, table design, machine guards, and the position of the cutting head all reduce practical clearance. The material may also need to sit on a sacrificial board, rubber support, or fixture, which consumes additional vertical space.
Assess the machine using the thickest expected stock plus the support arrangement. Then allow room for a controlled final pass. Running at the absolute depth limit leaves little tolerance for a bowed slab, a slightly worn blade, or a fixture that raises the workpiece. It also increases the chance that the blade exits the underside poorly, particularly where the support is interrupted beneath the kerf.
For a bridge saw, confirm whether the stated capacity applies to a vertical plunge cut, a full moving cut, or both. Some saws can plunge deeply at one point but lose practical capacity as the head travels because of guard clearance or table geometry. On rail-guided machines, verify clearance at both ends of the travel path. A high point in the table or a sagging support frame can affect a thick piece more severely than a thin tile because there is less spare depth.
Thickness changes the blade and feed relationship
A diamond blade does not cut stone by force alone. It must expose diamond segments at a rate that suits the material while carrying slurry away from the cut. As thickness increases, the blade remains in contact with the stone for longer and has less opportunity to cool between passes. A feed rate that produces an acceptable edge on a thin marble tile can overload the same blade in dense granite at a deeper cut.
Blade diameter should be selected with enough margin for the required depth, but a larger blade is not always a better blade. Larger diameters can impose higher rotational inertia and require a machine designed for the corresponding flange, guard, arbor, spindle speed, and motor load. Fitment must be verified as a system. Installing an oversized blade merely to obtain more reach can create vibration, inadequate guarding, or a speed mismatch that shortens blade life.
Blade bond and rim configuration should follow stone behavior. Softer and more abrasive materials tend to wear the bond differently from hard, dense materials. A blade that remains sharp in abrasive sandstone may glaze when used on dense quartzite, while an aggressive segmented blade can leave an unacceptable exit edge on a polished marble face. For visible edges, the final quality is often improved by reducing the last portion of the cut or using a finishing pass, rather than forcing one rapid full-depth pass.
Do not judge blade performance only by the presence of chips. A slow, polished-looking cut face can indicate glazing or insufficient feed. Dark marks, steam, unusual noise, and a curved kerf point toward other causes: inadequate water at the cutting zone, arbor runout, weak material support, a damaged flange, or a blade that has been overheated. Those conditions should be separated before changing machine size.
Machine rigidity matters more as the cut gets deeper
When a blade enters a thick slab, side pressure builds along a longer section of the rim. Any movement in the spindle, carriage, rail, table, or fixture is transferred into the kerf. The result may be a cut that begins square and drifts near the bottom, or a piece that appears straight from above but has a tapered edge. This is particularly troublesome when two cut edges must form a narrow seam.
Evaluate rigidity through the complete load path. The spindle should run smoothly with minimal perceptible movement; the blade flanges should clamp cleanly and remain undamaged; the head should travel without looseness; and the slab support should not flex as the cutting head passes. A heavily built frame does not compensate for worn carriage bearings or a table that is out of plane.
Long cuts deserve separate attention. A machine can make a satisfactory short sample cut while losing alignment over a full countertop length or architectural sill. Confirm rail straightness, bridge movement, and the ability to reference the workpiece consistently. Where the slab is repositioned between cuts, reliable fences, stops, or digital positioning are more valuable than a theoretical accuracy figure without a repeatable setup method.
Support and clamping differ by slab condition
Flat, sound slabs can often be held by their own weight with side stops and localized restraint, provided the table fully supports the area around the kerf. Fragile, fissured, resin-treated, or narrow offcuts need a more deliberate fixture. Vacuum pods, mechanical clamps, support bars, and sacrificial backing can all work, but their placement must avoid trapping the blade or allowing the two sides of the kerf to close against it.
Thick pieces present a different hazard: their weight can shift after the cut is nearly complete. A cut-off section that settles onto the blade can pinch the rim, damage the edge, or cause a sudden movement. Support both sides independently, especially for narrow strips, overhanging ends, and pieces with uneven undersides. A finishing cut should not rely on someone manually holding a heavy offcut in an unstable position.
Material condition matters as much as thickness. A 20 mm marble slab with a natural fissure can be more difficult to cut cleanly than a thicker, uniform granite piece. Veins may open during cutting, and mesh backing or resin can alter how water and slurry move through the kerf. Where a visible surface is vulnerable, test cuts should use material from the same batch and reproduce the intended orientation, support method, and edge condition.
Water management is part of capacity
Wet cutting is normally preferred for stone because water cools the blade and transports slurry away from the rim. For deep cuts, the question is not merely whether the machine has a pump. Water must reach both sides of the blade near the point of contact and continue to flow when the head is at the far ends of travel. Restricted nozzles, a clogged filter, a weak pump, or settled slurry in the tank can turn a capable saw into an inconsistent one.
Recirculated water requires attention to sediment. Abrasive slurry accelerates wear in pumps and can restrict nozzles. If the work involves light-colored or polished stone, contaminated water may also mark the surface or obscure the cut line. A practical arrangement provides settling space, accessible cleaning points, and a water path that does not flood the positioning references or electrical components.
Dry-cut equipment is used in some site conditions, especially for limited trimming with suitable dust extraction, but its depth and duty cycle must be assessed cautiously. The thermal load of a deep stone cut is far less forgiving than a brief shallow trim. When long, accurate, or repeated full-depth cuts are required, a wet cutting arrangement is generally easier to control for blade life and finish quality.
Compare the actual production task, not a single slab
A suitable machine must handle the largest piece, but it should also suit the normal sequence of work. A shop cutting many identical strips benefits from repeatable stops, programmable positions, or a reliable measuring system. A job involving occasional thick treads and frequent standard slabs may justify a bridge saw with adequate clearance and a separate method for exceptional block work, rather than choosing an oversized machine that is slow to set up for everyday cuts.
Consider the full work envelope: maximum slab length and width, loading direction, table access, head travel, and clearance to remove the finished piece. A machine can technically accept a slab while still creating awkward handling that damages corners or delays the next operation. The area around the saw needs space for incoming slabs, supports, offcuts, and safe movement of lifting equipment.
- For thin panels, inspect whether the table prevents vibration close to the cut line and whether the blade produces a clean exit on the finished face.
- For standard slabs, verify cut squareness over the longest relevant distance, not only at the start of travel.
- For thick sections, measure usable clearance with the intended blade, flange, fixture, and backing in place.
- Where finished edges are exposed, test the complete process: rough cut, final cut if used, handling, and any subsequent polishing or mitre operation.
Run a representative cut before final selection
A demonstration is meaningful only when it reflects the planned work. Use the actual stone type where possible, at the upper end of expected thickness, with the same blade category and support method. Observe the cut face, top and bottom edge condition, straightness, time required, water delivery, and slab movement. Then inspect the blade after several cuts rather than judging performance from a single fresh pass.
The final choice should leave usable depth and structural margin beyond the thickest routine piece, while preserving the accuracy and finish expected from the thinner work that may form most of the workload. That balance produces a cutting machine for stone that remains stable across changing slab thicknesses instead of performing well only under ideal conditions.
Technical Specifications
- What to verify before selecting a transformer manufacturer in the USAAuthor :Electrical Components Editorial Team
- How to choose a cutting machine for stone based on slab thicknessAuthor :Construction Materials Editorial Team
- When are porcelain tiles for outdoor spaces at risk of cracking?Author :Construction Materials Editorial Team
Expert Insights

Chief Security Architect
Dr. Thorne specializes in the intersection of structural engineering and digital resilience. He has advised three G7 governments on industrial infrastructure security.
Core Sector // 01
Security & Safety
- How to choose a cutting machine for stone based on slab thicknessAuthor :Construction Materials Editorial Team

- When are porcelain tiles for outdoor spaces at risk of cracking?Author :Construction Materials Editorial Team

- Marble Stone Price: What Changes Cost Across Grade, Finish, and Origin?Author :Construction Materials Editorial Team

- Marble vs Granite: Which Surface Performs Better Indoors?Author :Construction Materials Editorial Team

- Common Marble Problems and How to Prevent Stains and EtchingAuthor :Construction Materials Editorial Team

- Granite Countertop Selection: Finish, Density, and Daily WearAuthor :Construction Materials Editorial Team

- How Granite Performs in High-Traffic Commercial SpacesAuthor :Construction Materials Editorial Team